

Manufacturing asset management software keeps one record for every machine, tool, mold, vehicle and spare part a plant owns, and uses that record to plan maintenance, track where things are and report what each asset costs. Plants buy it when a spreadsheet can no longer answer simple questions: where is the spare motor, when was this press last serviced, and why does the same compressor keep stopping?
This guide covers what asset management in manufacturing involves, the problems it solves on the plant floor, how asset tracking in manufacturing works with tags and scanners, what to look for when you compare products, and how a plant usually gets started.
What is manufacturing asset management software?
Manufacturing asset management software is a system that records a plant’s physical assets, such as production machines, tooling, molds, dies, forklifts and utilities, and manages each one from purchase to disposal. It holds location, condition, maintenance history, spare parts and cost in one place, so maintenance, operations and finance work from the same list.
It overlaps with two other kinds of software that plants also shop for. A CMMS (computerized maintenance management system) focuses on work orders and preventive maintenance. A fixed asset register focuses on cost, depreciation and audits. Asset management in manufacturing needs both halves, because the machine that needs a bearing replaced is also a line on the balance sheet.
Manufacturing assets: what a plant needs to track
Manufacturing assets are wider than the machines on the line. A useful register covers:
- Production equipment: CNC machines, presses, injection molding machines, robots, conveyors and packaging lines.
- Tooling: molds, dies, jigs, fixtures and torque tools, which wear and often need calibration.
- Plant utilities: compressors, boilers, cooling towers, dust collectors and electrical gear that every line depends on.
- Mobile equipment: forklifts, carts, trailers and vehicles that move between areas or sites.
- Spare parts: bearings, seals, belts and motors held in storerooms for the machines above.
- IT and office equipment: shop floor PCs, scanners, printers and laptops.
Each group needs different things. A press needs hour-based service plans. A mold needs a location and a shot count. A spare motor needs a reorder point. Good software lets you hold all of them in one register while treating them differently.
Why manufacturing needs asset management software
The case for asset management in the manufacturing industry comes down to a handful of problems that get worse as a plant grows.
Spreadsheets fall out of date
A spreadsheet works for a small shop with one person maintaining it. Once several people edit it, copies drift apart, formulas get overwritten, and nobody can say who changed a location or when. The data is wrong in exactly the places where you need it, such as an audit or a breakdown at 2 a.m.
Unplanned breakdowns stop the line
When a machine fails without warning, the repair is only part of the cost. Operators stand idle, orders slip, and parts are rushed in at a premium. Machines that miss their scheduled service fail more often and wear out sooner. Preventive maintenance, planned by calendar, run hours or cycle counts, is the main defense.
Missing spare parts turn short jobs into long ones
A breakdown that needs an inexpensive bearing can stop a line for a day if the bearing is not on the shelf. Plants with several storerooms often have the part somewhere, but nobody can see it. Stock levels, reorder points and a link between parts and the machines that use them fix this.
Assets go missing or become ghost assets
Portable tools, test equipment and spare motors move between shifts, lines and sites. Without a record of who has what, they get lost or walk out. The opposite problem is the ghost asset: a machine still on the books, still being depreciated, that was scrapped years ago. Both show up as soon as an auditor asks to see something.
Audits and compliance need records you can show
Auditors check the fixed asset register against the floor. Safety inspectors want proof that lockout, inspections and certifications were done. Quality standards such as ISO 9001 expect equipment and calibration records. If those records live in binders and personal spreadsheets, every audit becomes a scramble.
Decisions get made on guesses
Should you repair the old compressor again or replace it? Which line has the worst downtime? Without maintenance cost and failure history per machine, these become arguments rather than decisions.
Asset tracking in manufacturing
Asset tracking in manufacturing is the part of asset management that answers “where is it and who has it?” Every asset gets a unique number on a label, and scanning that label updates its record. The method depends on the asset.
| Tracking method | How it works | Best for in a plant |
|---|---|---|
| QR code or barcode label | Scanned with a phone or handheld scanner | Machines, spare parts, tools, shop floor IT |
| Handheld RFID | Reads many tags at once without line of sight | Counting a storeroom or tool crib quickly |
| Fixed RFID reader | Records tags passing a doorway or gate | Tools and equipment leaving the crib or the dock |
| GPS tracker | Reports location outdoors | Trailers, yard vehicles, generators |
| BLE tag | Places an asset on an indoor floor plan | Mobile equipment in large buildings |
Most plants start with QR or barcode labels on everything and add RFID or GPS only for the assets that move often or cost the most. A label costs almost nothing, while a reader or tracker needs hardware and power. Our guide to RFID asset tracking explains when RFID is worth it.
Tracking pays off in three places. Technicians find tools and spares without searching. Physical counts become a walk with a phone instead of a week with clipboards. And the register stays close enough to reality that finance can trust it.
Benefits of asset management in manufacturing
When the register, the maintenance plan and the stock list share one record, a plant gets:
- Less unplanned downtime, because service falls due by hours or cycles and breakdowns are reported against the machine.
- Longer asset life, because machines are serviced on time and their history shows wear before it becomes failure.
- Fewer lost tools and spares, because each item has a location and a custodian.
- Faster audits, because counts are scanned and every move, disposal and change has a history.
- Better repair-or-replace decisions, because maintenance cost and failures are recorded per asset.
- Lower stock costs, because reorder points replace guesswork and parts are visible across storerooms.
What to look for in manufacturing asset management software
Use this checklist when you compare products. The questions on the right are the ones to ask in a demo.
| Capability | Why it matters in a plant | Ask the vendor |
|---|---|---|
| Asset hierarchy | Lines, stations and components need a parent and child structure | Can I build plant, line, machine and component levels? |
| Meter-based maintenance | Machines wear by hours and cycles, not by calendar | Can a plan fall due by run hours or whichever comes first? |
| Failure codes and history | Reliability reporting needs something to group by | Can technicians close a job with what failed and why? |
| Spare parts and reordering | A missing part stops a line | Are parts linked to machines with reorder points by storeroom? |
| Labels and scanning | The register is only as current as the last scan | Can I print QR, barcode and RFID labels from the record? |
| Offline mobile app | Plant floors have dead spots | Does the app scan and record without a signal? |
| Lockout and permits | Isolation has to be recorded before work starts | Can a job be blocked until a permit is in force? |
| Depreciation and disposal | Finance needs the same record as maintenance | Can it run book and tax depreciation and record disposals? |
| Multi-site access | Each plant should see its own assets | Can access be limited by site? |
How to roll out asset management in a manufacturing plant
Most plants go live on one line or area first, then add the rest.
- Import the assets. Load the machines for one line from your spreadsheet, with make, model, serial number, location and criticality.
- Tag them. Print labels and fix them to each machine, tool and spare. Start with the most critical equipment.
- Load the maintenance plans your technicians already follow, starting with hour-based services.
- Turn on failure codes for breakdown jobs, so history builds from the first week.
- Set reorder points on the spares that have stopped the line before.
- Run a first count on that line to prove every tag scans to the right record, then move to the next area.
Discrete and machining plants
Start with CNC machines, presses and compressors. Hour-based compressor services and quarterly machine PM go in first, and failure codes on breakdowns give the reliability reports something to count within a few months.
Automotive and assembly plants
Presses and robots run on cycle counts and run hours. Torque tools carry calibration schedules. Line stops are planned as shutdowns, so parts and permits are ready before the window opens.
Multi-plant groups
Each plant runs its own storerooms and technicians. Group engineering compares uptime, backlog and spend across sites, and parts can move between plant storerooms.
How Asset Infinity handles manufacturing asset management
Asset Infinity keeps every machine in one asset register with its site and location, parent asset, owning department, cost center, criticality, manufacturer, model, serial number, warranty expiry, expected life, purchase cost and custodian. A spreadsheet imports as a CSV or Excel file, and every row is checked before anything is written.
On the floor, the system works like this:
- Tag and scan. The label designer prints QR, barcode and RFID labels, as ZPL for thermal printers or as PDF. Technicians scan a machine in the iOS or Android app, which works offline, to open its record or raise a job. See asset tags.
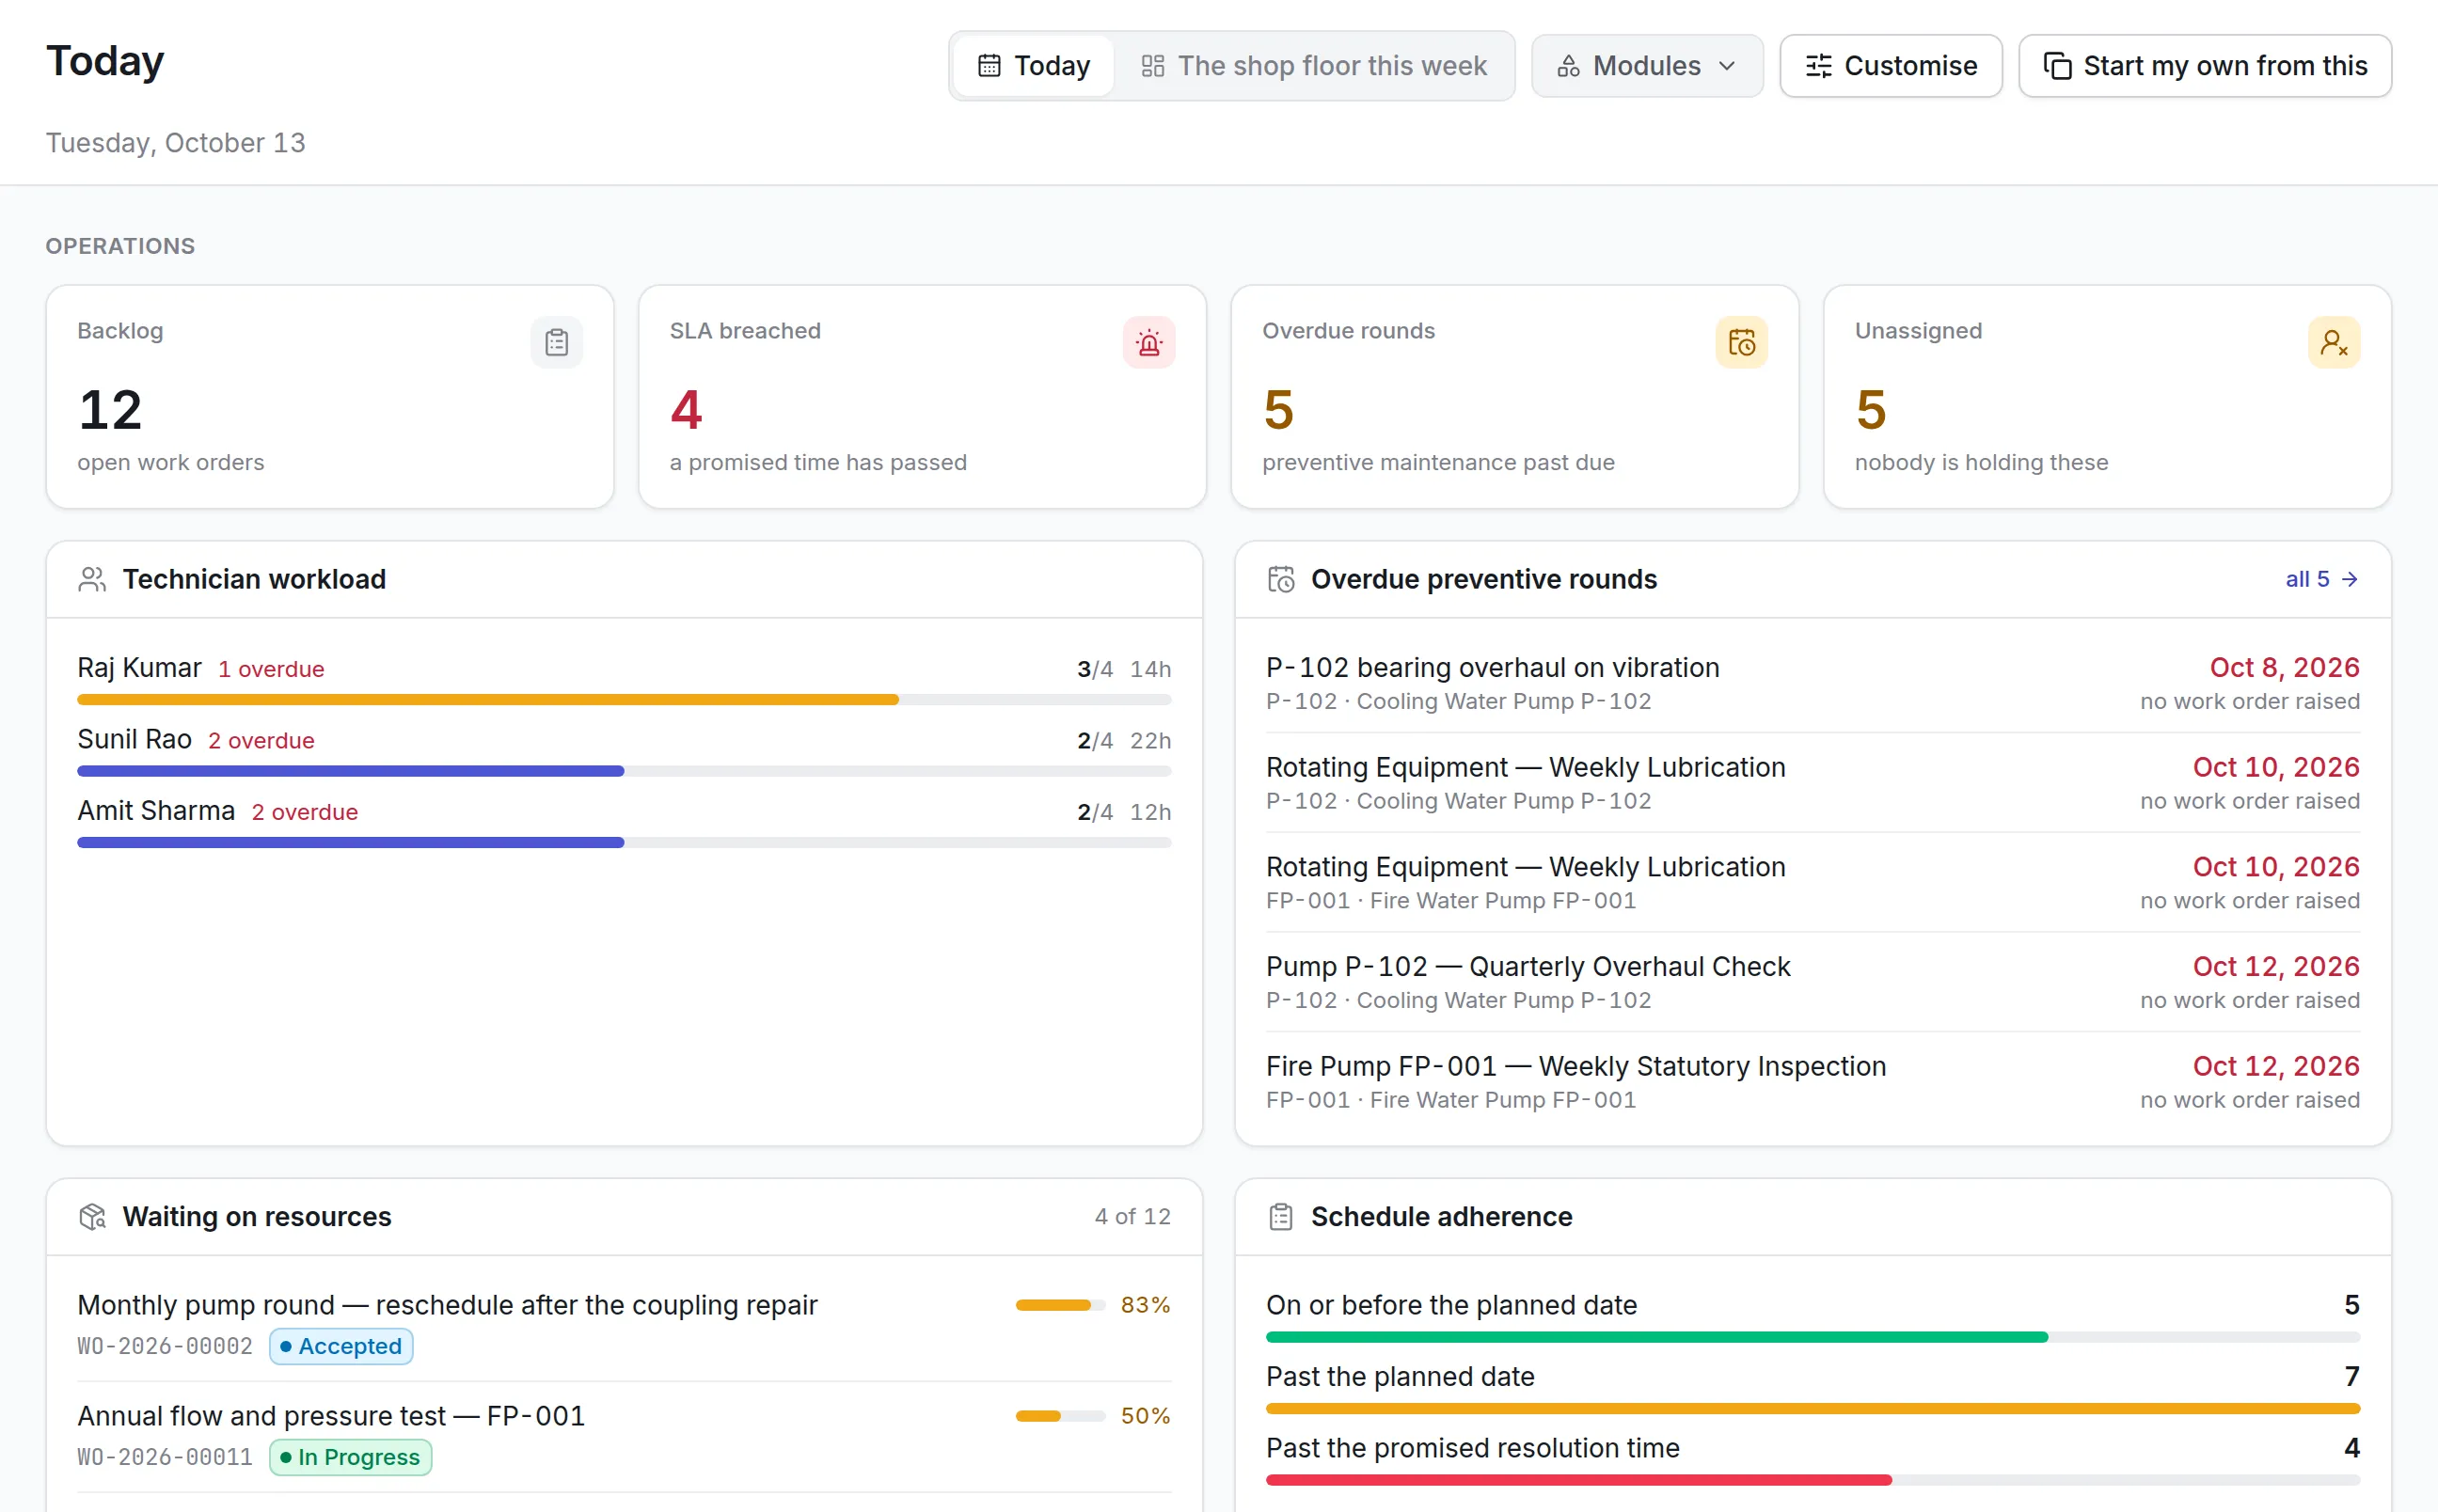
- Report breakdowns. Operators report a fault from the web or by email, and the job carries its failure code and response clock.
- Plan prevention. Plans fall due by calendar, run hours, cycle counts or a sensor limit, whichever comes first. See preventive maintenance software.
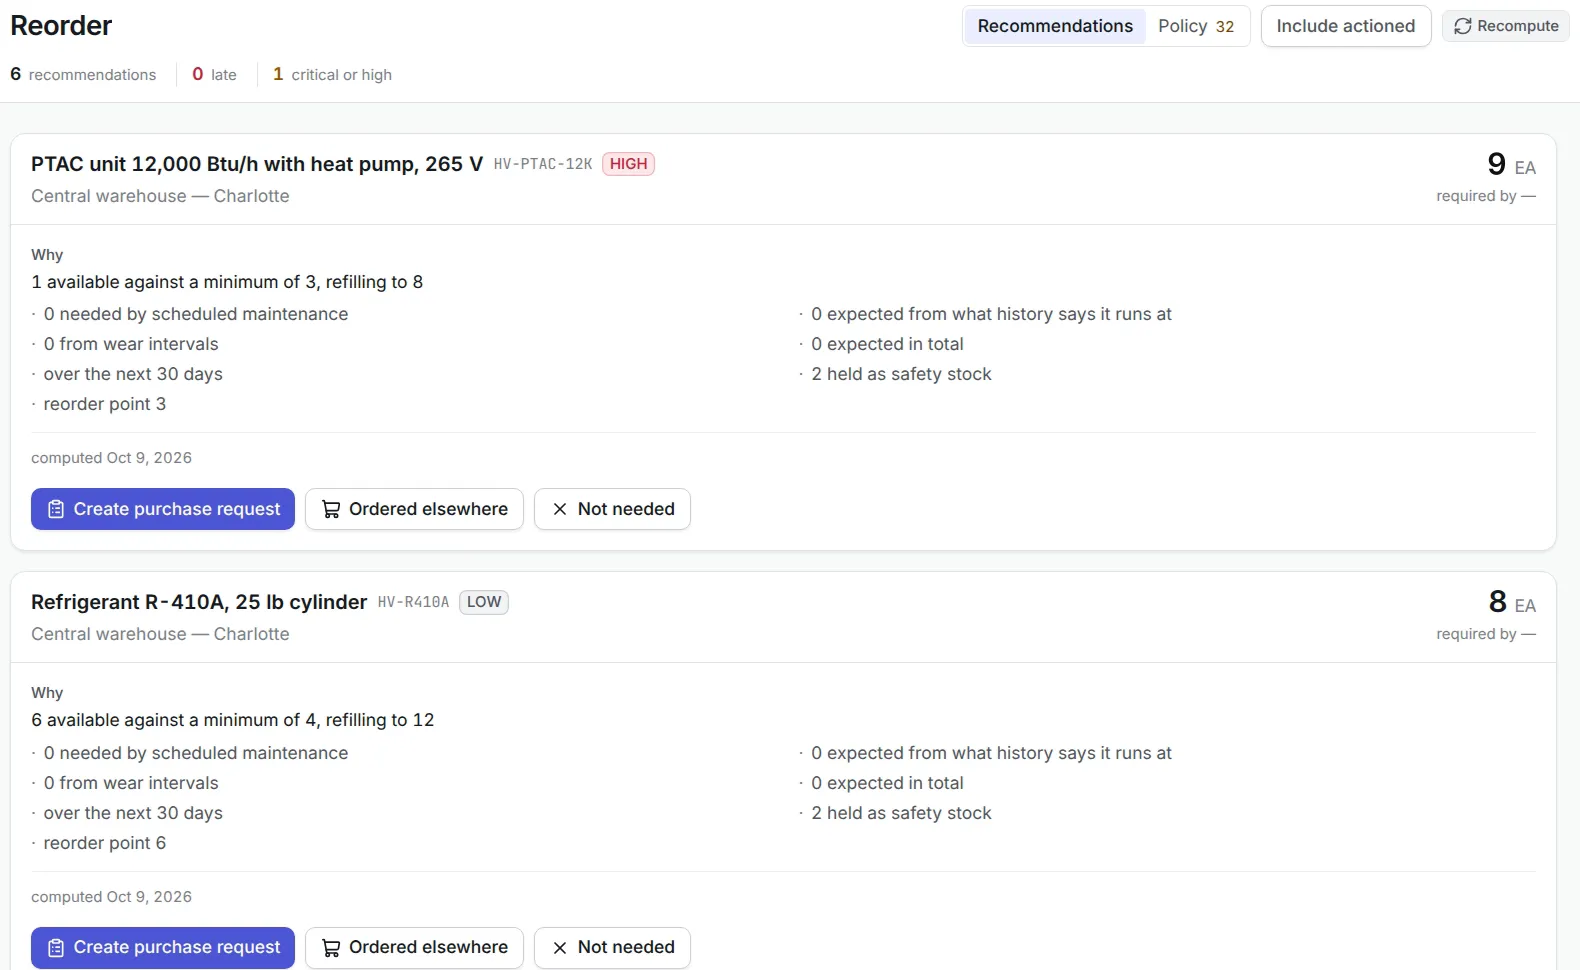
- Keep spares on the shelf. Parts carry minimums and reorder points by storeroom, and shortfalls turn into purchase requests. See parts inventory management.
- Measure reliability. Availability, MTBF, MTTR and maintenance cost are worked out for every asset, and repeat faults are flagged for root cause analysis.
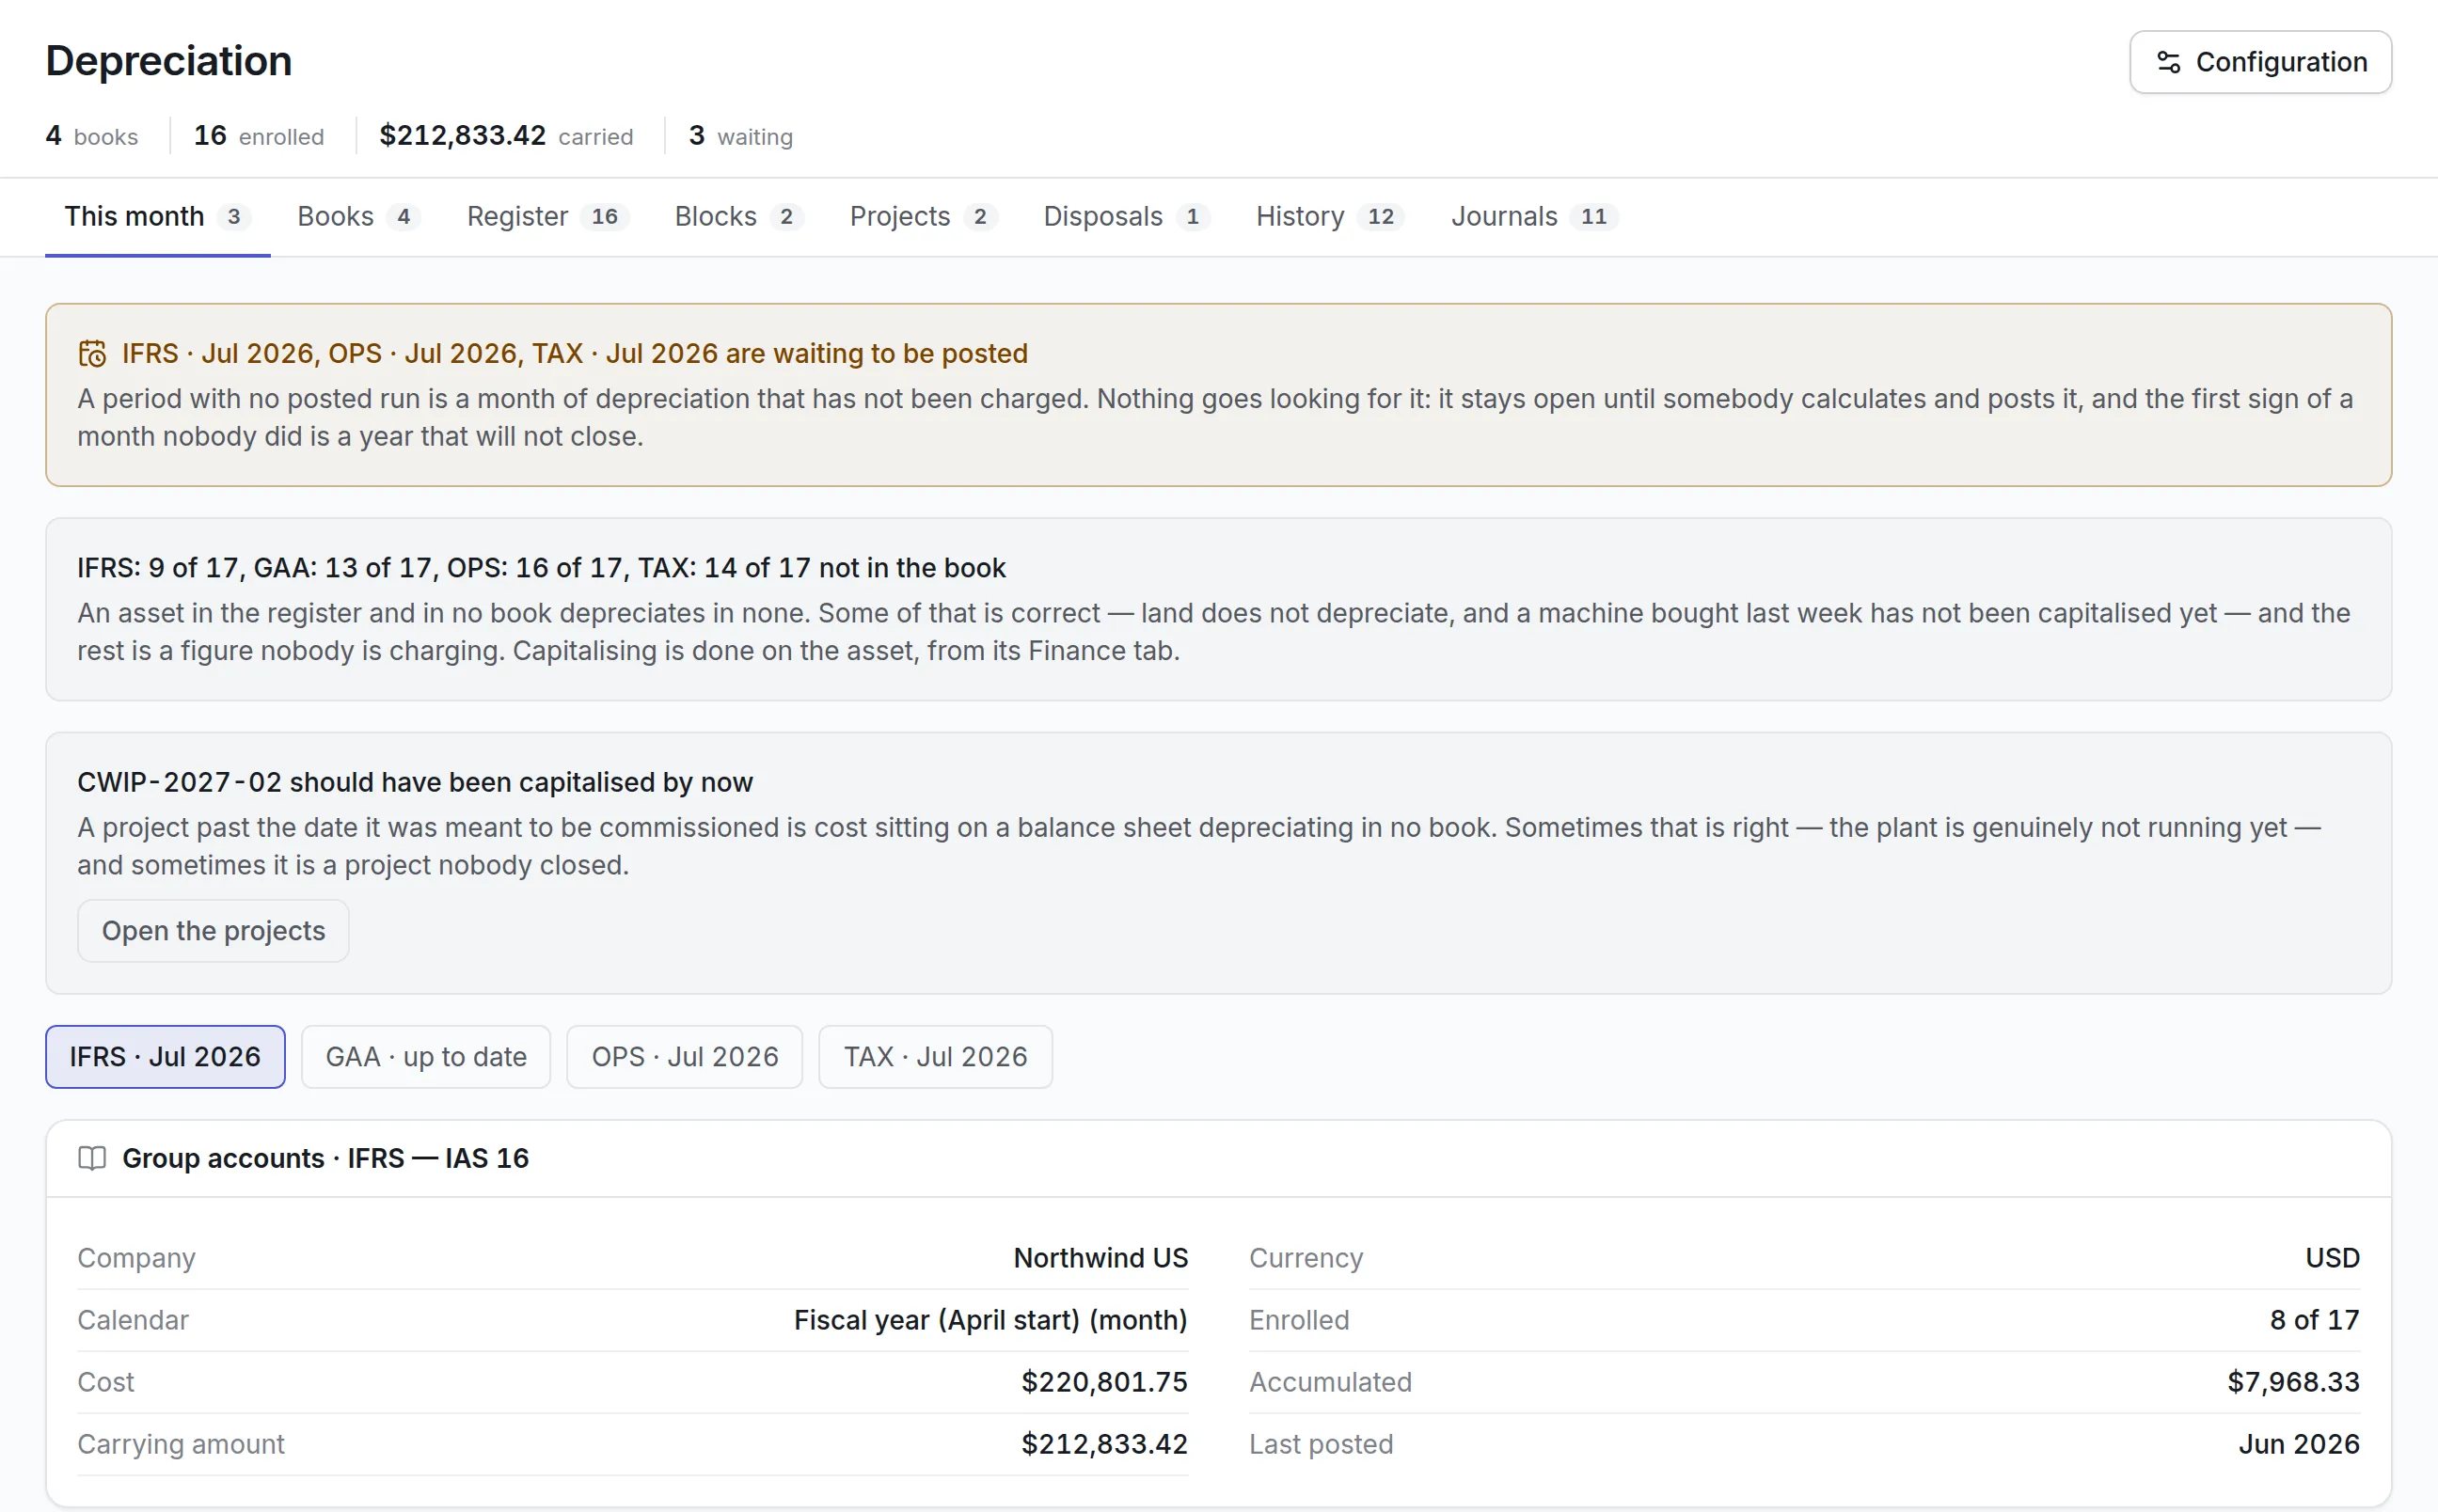
- Close the books. Depreciation runs in more than one book, such as statutory and tax, and disposals record the reason, sale price and gain or loss.
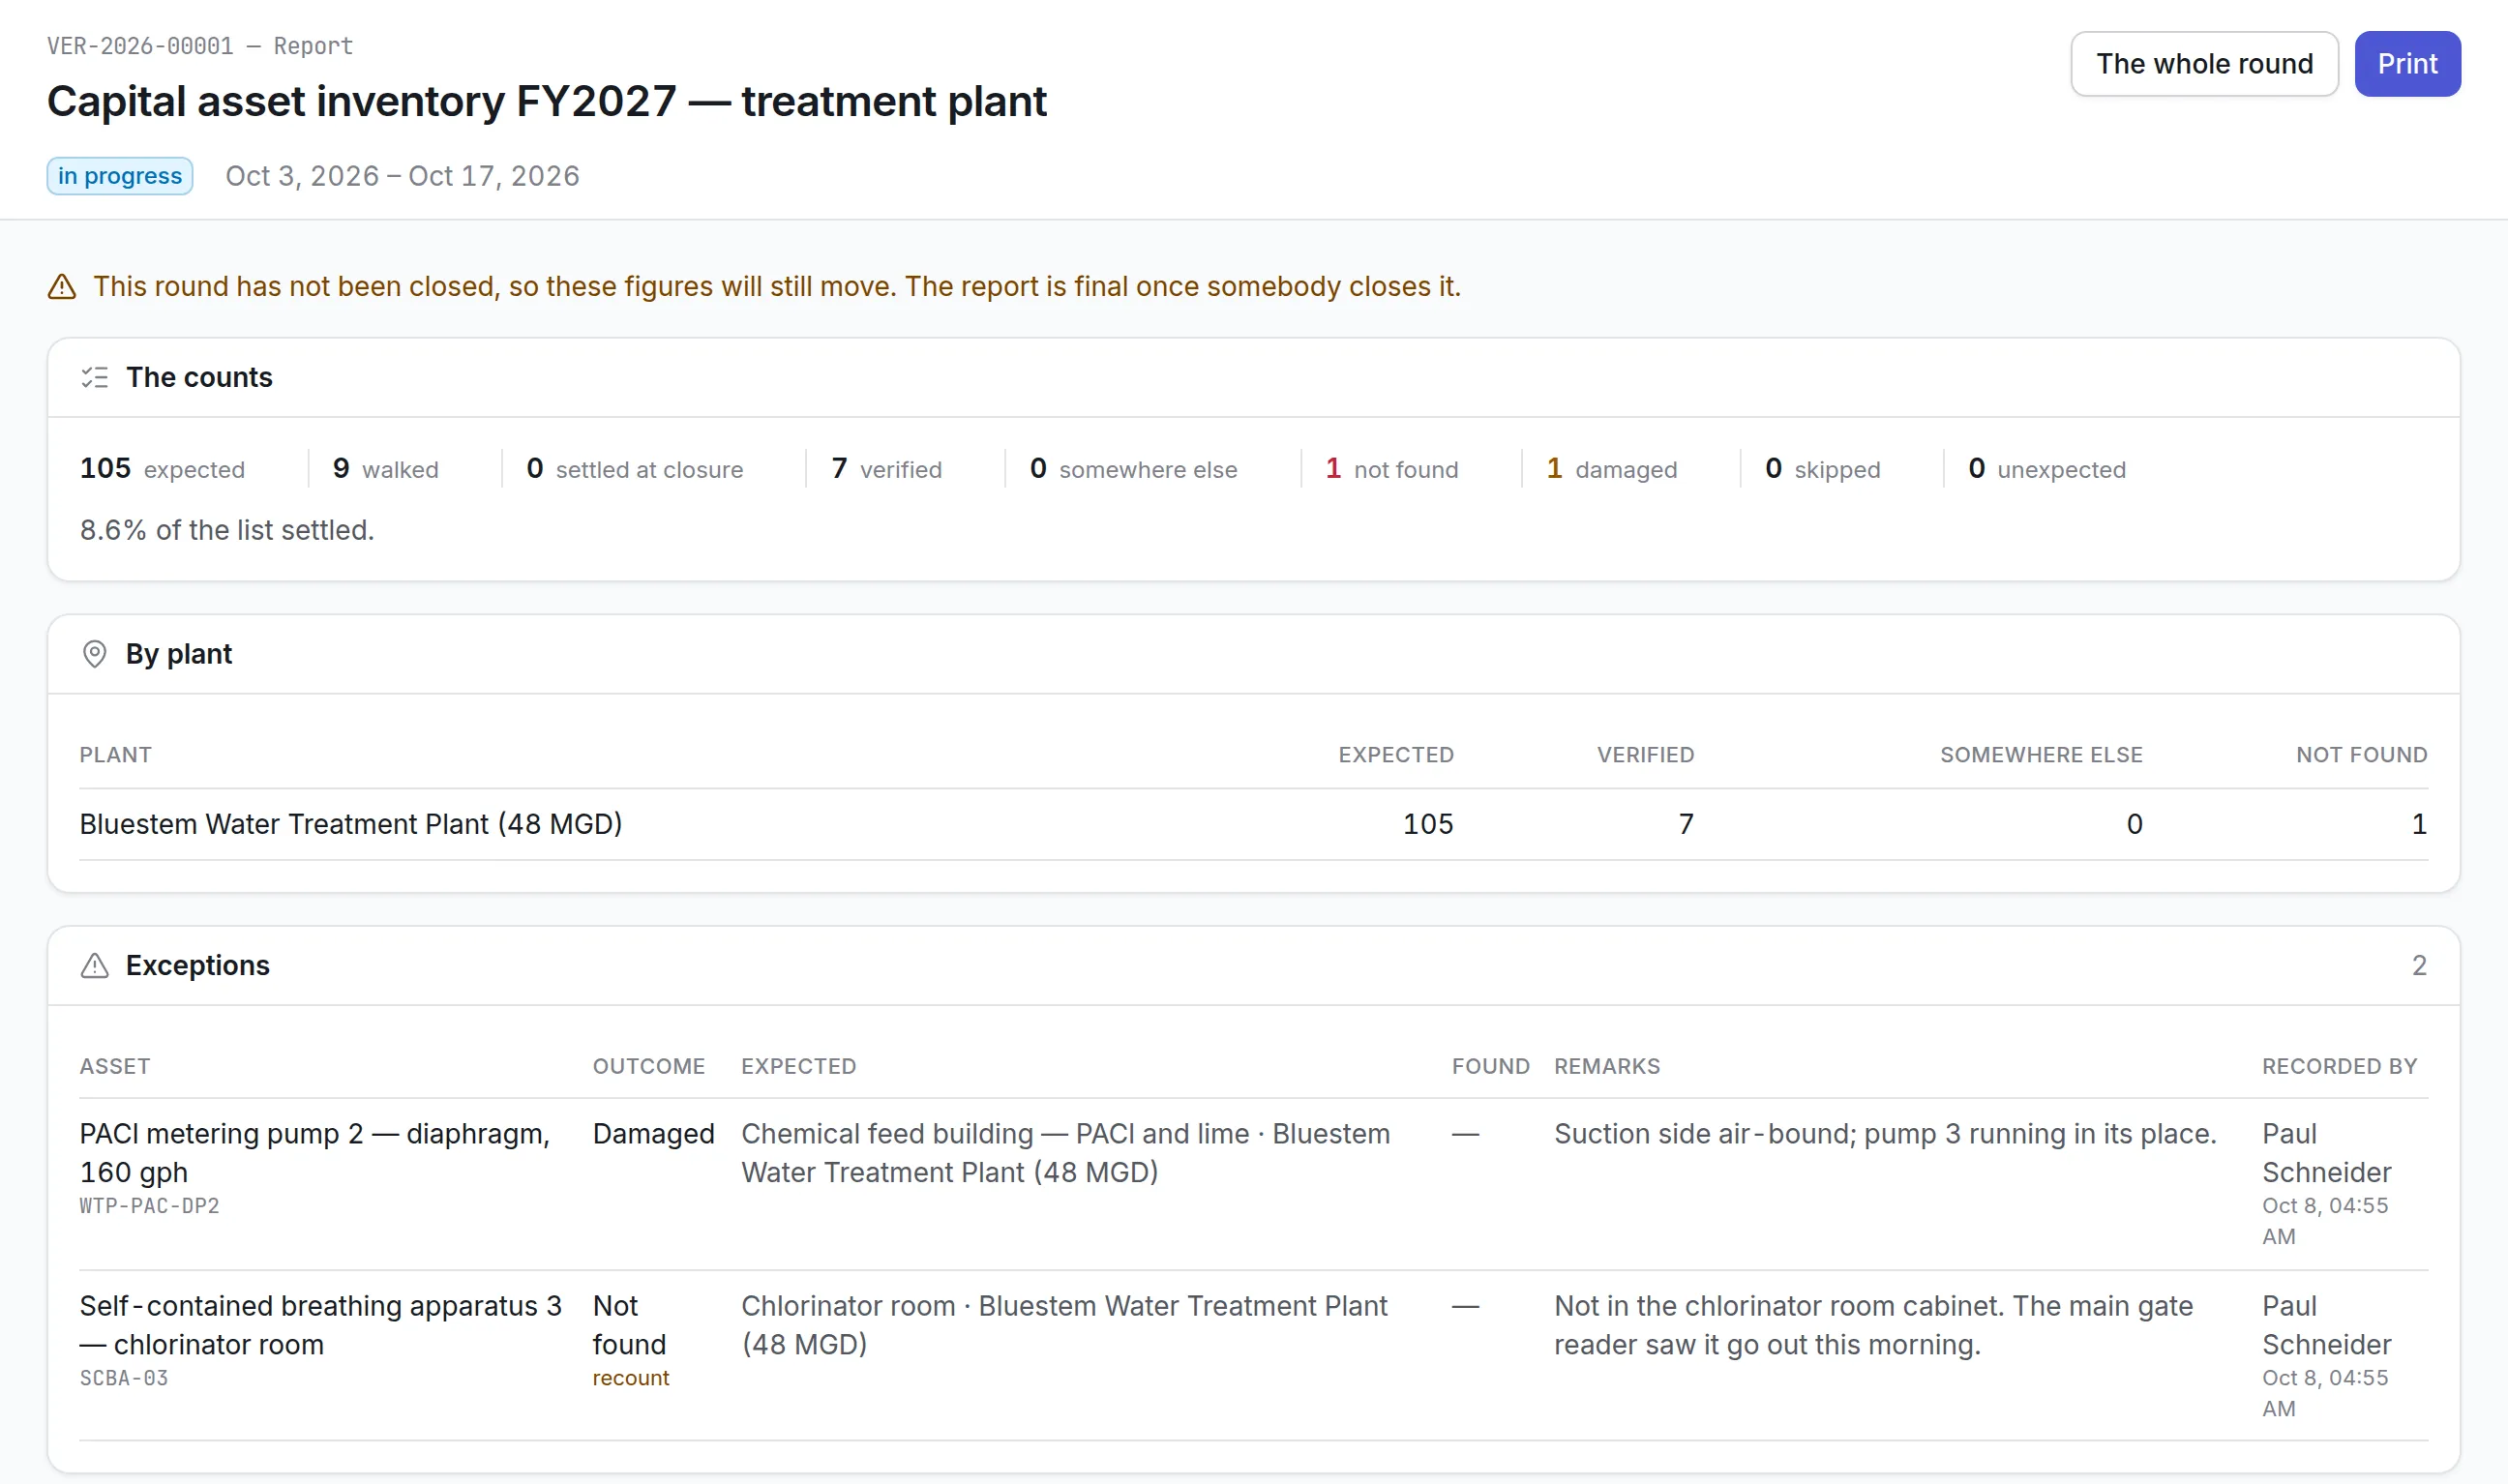
Statuses run from Planned and Operational through Under Maintenance and Breakdown to Retired and Disposed, and the status history is kept, so downtime is on record. Verification rounds are walked with the mobile app, and each asset is recorded as verified, moved, damaged or not found.
The manufacturing maintenance software page shows the plant setup in detail, and a manufacturing asset tracking case study shows one manufacturer’s rollout. To see it with your own equipment, book a demo.
Frequently Asked Questions
What are manufacturing assets?
Manufacturing assets are the physical things a plant uses to make its products: production machines, tooling such as molds and dies, plant utilities, forklifts and vehicles, spare parts and shop floor IT. Raw materials and finished goods are inventory, which is usually managed separately.
What is the difference between a CMMS and manufacturing asset management software?
A CMMS focuses on maintenance work: work orders, preventive plans and technicians. Manufacturing asset management software also covers tracking, custody, counts, depreciation and disposal. Many plants want both in one system so maintenance and finance share the same asset record.
Is asset management software only for large manufacturers?
No. A small shop with one site gains from scheduled maintenance and a register it can trust as much as a large group does. Small plants usually start with labels, a register and preventive maintenance, and add reliability reporting later.
Can manufacturing asset management software run in the cloud?
Yes. Asset Infinity runs in the cloud, so plant staff can reach it from a browser or the mobile app. The same product can also be installed on your own servers if your plant needs that.